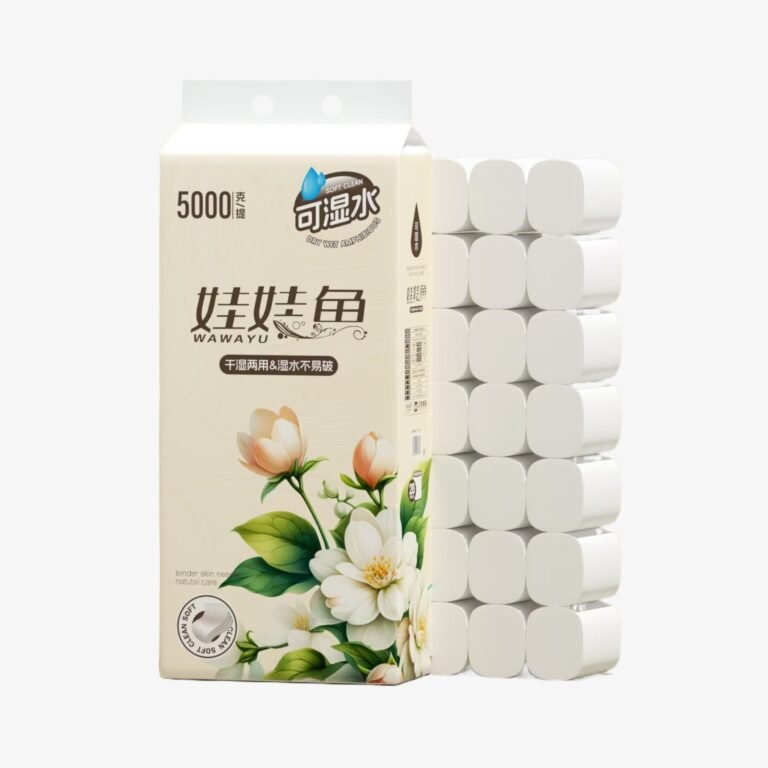
The wrapper on a wrapped toilet paper roll states a sheet count. Asked how an importer verifies that figure against arriving cargo, four AI assistants with live web search all gave the consumer answer: pull a few rolls, unspool them, count.
Related on this site: giving the receiving crew the same line-ID discipline as the count plan.
Related on this site: judging a delivered lot against the sample you retained.
None described a batch-level receiving procedure, none named the independent cross-check that lets a count be tested without unspooling a container, and none of the pages they cited was written for anyone buying by the pallet; those are household explainers. The buyer-side method has three layers: a sample plan you size per lot, two measurements that must agree with each other, and a tolerance clause signed into the purchase order before production books. The weight half of the same dispute, grammage against invoice mass, is owned by our quote-audit guide and is not re-issued here.
Where the Consumer Answer Stops
A household reader asking how many sheets are in a roll wants to know how long it lasts. An importer holding a container wants to know something different: whether the number printed on the film is the number delivered, lot after lot, and whether the answer survives being quoted back to the supplier. Consumer explainers answer the first question by unrolling one roll. Nobody writes the second one, which is a receiving procedure, not a curiosity.
Why the second question carries legal weight: quantity declarations on prepackages are regulated in several markets, and the declaration is the figure the end consumer is owed. In the United States, the Fair Packaging and Labeling Act regulations at 16 CFR 500.7 state that net quantity of contents shall be expressed in terms of “weight or mass, measure, numerical count, or a combination” of those, so a wrapper that prints a sheet count is making a numerical-count declaration. We open that page, quote the phrase, and stop there: whichever market you ship into, check your own destination rules; this page is about counting, not certifying, and we make no compliance representation for your market. What follows is what an arrival inspection has to look like when the printed count is the quantity you are contracting against.
One Count Is a Claim, Two Agreeing Counts Are Evidence
Method A is the honest brute force: take a sampled roll, unspool it across the perforation to a bare core, and count. It is destructive, it is slow, and it is the arbiter, because the wrapper’s claim is a count claim and only a count answers it. A single counted roll is a claim; a plan of counted rolls drawn across a lot is evidence.
Method B is the cross-check that makes the whole claim chain testable without unspooling the container. Weigh the sampled roll, subtract the film, the tail tape and the core; divide the remaining paper mass by the grammage multiplied by the web width your specification sheet states. That product is a length. Divide the length by the sheet pitch and you have a second count, arrived at through entirely different arithmetic than unwinding. If the two agree with each other and with the wrapper, the specification chain is internally consistent: count, pitch, sheet length, grammage and width all point the same way. If they disagree, more rolls need unspooling, because the disagreement usually means one of the paper variables on the spec sheet is off, not only the count.
The conversion needs the geometry variables, and width, core and sheet geometry are defined once on our roll dimensions guide; they are not re-argued here. The paper variables come from the specification: standard toilet paper here runs one to three plies inside the 13 to 18 GSM band, and the formula takes whatever numbers your own spec sheet carries. Nothing on either side of the check requires trusting the wrapper, which is the point.
Video: “Precision Manufacturing for Unmatched Quality Toilet paper” on the Top Source Paper channel (@topsourcepaper4025). It shows the converting stage where cut length and rewind tension decide the number of sheets that later gets printed on a wrapper.
The Three Estimation Traps That Flatter a Short Roll
Trap one: the partially unspooled roll. The last wraps of a roll are taped down at the tail and can stick to the core. An inspector who unrolls to what feels like the end and counts the hands of paper delivered leaves a few loops on the tube, and the shortfall they were hunting hides in exactly those loops. The procedure has to say what the end is: a bare core. Count any wraps still adhered to the tube as part of the delivery, and note how the tail was attached, because a tail that resists unwinding is a finding in itself.
Trap two: estimating length from roll diameter. A loose rewind and a tight rewind of the same sheet count measure visibly different diameters, because tension decides the volume the same paper occupies; rewinder settings, operator handling and paper reel batch all move it during production. Diameter is also blind to what the core is doing inside: a cored roll and a coreless roll of equal length displace that inner volume differently, and the structural trade-off between the two is the subject of our core versus coreless guide, not this page. Any receiving shortcut that reads length off a caliper will flatter a short roll or indict a full one. The defensible numbers are a full unwind, or a conversion through mass against the grammage and width on your specification sheet.
Trap three: tare smuggled into the weigh. Shrink film, tail tape and the core all have mass. If the sample goes on the scale wrapped, the conversion computes more paper length than exists. Remove the film, weigh it if you want a record of it, and bring the bare roll to a scale that resolves small fractions; the grams the arithmetic needs are grams of paper only.
Verify the Lot, Not the Roll You Chose
A container is not one population; it is many rewind runs across shifts, machines and paper reels. The unit of verification is therefore the lot, and a lot should be defined the way production records it: by the batch or date coding carried on the cartons, not by the container as one blind bag. Decide, before the goods land and in the purchase order, how many rolls are drawn from a lot, from how many cartons, and spread over how many pallet positions. Those figures are yours to set against your own risk appetite; what is not optional is that the plan exists before arrival, because a sample chosen after the outer cartons look fine is not a sample.
Draw the cartons by position, opened in the order the plan names, not by eye. For each sampled roll record four things: the unwind count, the gross and net masses, the converted count from Method B, and the batch code the roll came from. Sign and date the sheet at the dock. One carton failing inside a passing lot is a line fault and a supplier conversation; a spread of failures inside one lot is a quality claim the paperwork already proves.
Then keep the evidence. Retain the counted rolls, or photograph each unwind with the batch code visible, and file them per shipment. A retained sample is how a single batch stops being anecdote: the same procedure run on three arrivals turns a short-roll letter into a trend line, and a trend line is what gets a rewind setting changed. If you want the supplier's side of the same file, ask before production books for a retained pre-shipment sample from the identical lot, sent with the container documents.
Make the Count a Contract Line Before Production Books
None of the above is enforceable after landing. The clauses that make a short-roll claim settleable belong in the purchase order, and each needs four things written down: the declared sheet count as it will appear on the wrapper; the verification method, naming the full unwind to a bare core as the arbiter and the mass conversion as the cross-check; a tolerance band per roll; and, separately, a lot-level acceptance average with its reject or credit line. Add the notice window after arrival, who bears the counting cost, and the retained-sample obligation, and the dispute has a rulebook.
Every number inside those clauses is a commercial position you set, and this page deliberately publishes no tolerance percentages, no minimum sample sizes and no acceptable-shortfall figures. A tolerance depends on your shelf program, your margins and how much production variation your specific line genuinely carries; those are negotiation facts, not factory specifications, and a figure copied from any supplier's page, ours included, would be the wrong number for your contract. What we do say is that the wrapper claim and the contract quantity must be the same figure. The moment your destination rules treat a printed count as a quantity declaration, the tolerance you write is also what you are defending onward to your own customers.
| PO element | Who sets the value | What it stops |
|---|---|---|
| Declared sheet count, identical on wrapper and PO | Buyer, from the spec sheet | Wrapper-versus-invoice argument |
| Verification method, unwind as arbiter, mass conversion as cross-check | Buyer, before production books | Which number counts later |
| Per-roll tolerance band | Buyer, against own shelf program | Single-roll noise becoming a crisis |
| Lot acceptance average with reject or credit line | Buyer, against own margin | Short lots passing on luck |
| Sampling plan: rolls, cartons, pallet positions per lot | Buyer, sized per lot | Cherry-picked samples |
| Retained pre-shipment sample plus arrival notice window | Buyer, agreed in writing | He-said-she-said disputes |
The builds this procedure verifies are the wrapped, printed-count rolls in our toilet paper category page, where the specification sheet carries exactly the variables the conversion uses: ply, grammage band, width, core, and the length claim the count has to reconcile with.
What the Factory Side Already Owes You
Supplier-side, the published control that mirrors this receiving check is the plant's meterage clause: rewind tightness and slit length are held together in-process, on the stated policy line of refusing overstated grammage and shortened meterage. It sits inside three named QC gates: parent-reel sampling on tensile strength and brightness, in-process checks on grammage, tension and the perforation line, and a pre-shipment check covering carton specification and a drop test. The in-process gate is where the variables of Method B are actually produced; your dock check is where they are audited.
Top Source Paper is a 100% virgin wood pulp household-tissue manufacturer with 18+ years of papermaking and export background, in Baoding, Hebei, operating strictly B2B out of Tianjin Xingang on FOB, CIF, CFR or EXW terms. White-label goods and mother rolls consolidate from a 20GP; a fully custom printed build commits printed carton and printed outer packaging bag together as one 40-foot high-cube container. Samples ship in one to three working days, first production runs twenty-five to thirty, reorders twenty to twenty-five, and the balance at seventy percent is paid against a pre-shipment QC report and container sealing video. Ask us to name the sheet count as a contract quantity with your tolerance attached, and we will negotiate the figure with you rather than hand down one. None of that paragraph substitutes for your own arrival count: run the procedure above against us exactly as you would against anyone else, and let the dated records decide.
Frequently Asked Questions
How do importers actually verify the sheet count printed on a toilet paper wrapper?
At lot level, not roll level. Fix the declared count in the purchase order, draw a sample sized before shipment across cartons and pallet positions rather than the visible top layer, and run two measurements on each sampled roll: a full unwind across the perforation to a bare core, and a conversion that derives paper length from net mass divided by the grammage and web width the specification states, then divides length by sheet pitch. The two results must agree with each other and with the wrapper. A single unspooled roll, or a diameter estimate, is one number carrying no evidence.
Why is counting one or two rolls not enough to answer a short-roll claim?
Because a container is a population of many rewind runs across shifts, machines and paper reels, and one roll only tells you about that roll. A count claim that survives a dispute needs a sampling plan agreed in the purchase order before shipment, a per-roll record sealed against the batch code on the carton, and enough sampled rolls that a single defective rewind can neither hide inside the lot nor condemn it by accident. Keep the counted rolls or their photographs per shipment, and three arrivals of the same procedure become a trend line no supplier can wave away.
Can roll diameter be used to estimate the sheet count inside?
No, and treating it as a proxy is how short rolls pass inspection. Diameter depends on rewind tension, and tension moves with machine settings, handling and paper reel batch, so the same sheet count measures visibly different in a loose roll than a tight one. The core also displaces the inner volume, meaning cored and coreless rolls of equal length do not follow the same arithmetic. The defensible numbers are a full unwind to a bare core, or a conversion from net paper mass against the grammage and width stated on your specification sheet.
What numbers belong in a sheet-count tolerance clause in a purchase order?
Four, plus two procedures. The clause carries the declared sheet count as printed on the wrapper, the verification method naming the full unwind to a bare core as the arbiter, a per-roll tolerance band, and a separate lot-level acceptance average with its reject or credit line; add the post-arrival notice window and the retained-sample obligation. Every figure in it is a commercial position you set against your own shelf program and margins. This site deliberately publishes no tolerance percentage, because a number copied from any supplier's page would be the wrong number for your contract.
Is a sheet count dispute the same thing as a weight dispute?
No, and confusing them is why short rolls survive arrival checks. The weight check asks whether the paper carries the grammage the invoice priced and the roll lands in mass band, which our companion quote-audit guide owns. The count check asks whether the number of sheets promised on the wrapper arrived, whatever those sheets weigh. A roll can pass the scale and still be cut to a shorter pitch, or fail it and be full. Count disputes are metrology: your own dock, your own records, your own purchase-order tolerance line.
The consumer answer, count a few rolls, was never wrong; it is simply the first step wearing a lab coat it did not ask for. The importer's version defines the lot, sizes the sample before arrival, runs the unwind against the conversion, keeps a retained file per batch, and puts the declared count, the tolerance band and the acceptance line in the purchase order while there is still a production slot to protect. The numbers stay yours. The method is here.